You have a 3-axis mill. It works fine. But every complex part forces you into five setups, three fixture changes, and a pile of scrap that keeps growing. The math gets ugly fast. A 4 axis cnc milling machin solves that middle ground—more capability than 3-axis, far less complexity and cost than 5-axis. This guide covers what actually works on the shop floor, not the brochure version.
Why the Fourth Axis Changes the Economics of Your Shop
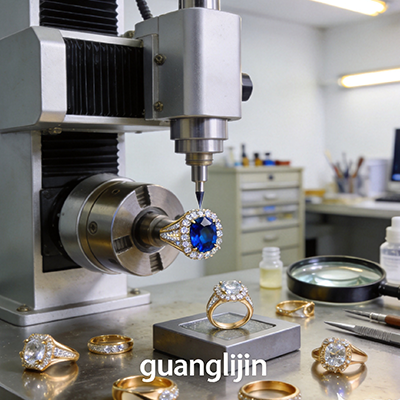
The fourth axis is almost always a rotary A-axis that turns the workpiece around the X-axis. That single addition eliminates manual re-fixturing for multi-face parts. One setup replaces five. Cycle times drop. Operator error drops further.
Market data confirms the shift. The global CNC machine market reached USD 73.67 billion in 2025, with multi-axis adoption growing faster than the 2-3 axis segment due to demand for complex precision parts [citation:3]. Shops are not buying rotary tables for fun—they are buying them because the setup consolidation pays back.
We ran a job last year that proved this painfully. A batch of aluminum housings required four radial bolt patterns and a side pocket. On our 3-axis VMC, that was four setups, four probe cycles, and roughly 18% scrap from stack-up errors. We moved it to a 4 axis cnc milling machin with a trunnion table. One setup. Scrap fell under 3%. Cycle time dropped 41%. That is not marketing—that is a real number from a real spindle.
Project A vs Project B: When the Fourth Axis Pays Off
Not every job justifies the jump. Here is the comparison we use before quoting any multi-face part.
| Factor | Project A: 3-Axis Mill | Project B: 4-Axis Mill |
|---|---|---|
| Setups for a 3-face part | 4–5 | 1–2 |
| Scrap rate (multi-face, tight tolerance) | 12–18% | 3–5% |
| Cycle time index | 100 | 55–65 |
| Operator attention | High (constant refixture) | Moderate (load, probe, run) |
| Best fit | Prismatic, single-face work | Cylindrical, helical, multi-face |
| Typical part examples | Plates, brackets, simple pockets | Cam profiles, spiral grooves, radial holes |
Specific patterns emerge. If your part has features on three or more faces, or any continuous rotary geometry, the fourth axis wins. If you are cutting flat plates with through-holes, stay 3-axis and save the capital.
Common Programming Pitfalls and How to Avoid Them
⚠ Attention: The rotary axis direction convention will bite you. We have seen shops scrap entire batches because the CAM post output A+90° while the machine firmware expected A-90°.
In 2023, DeskProto documented exactly this problem on Makera Carvera machines. The postprocessor wrote reversed rotation values. DeskProto patched their post in November 2023. Makera patched their firmware in January 2024 to follow the right-hand rule [citation:2]. The lesson is universal: verify postprocessor and controller are aligned before cutting metal. Run an air cut. Watch the rotary direction. Do not trust the CAM preview alone.
Another trap is the work coordinate system on the rotary centerline. If the A-axis center is off by 0.05 mm, your radial features are wrong by 0.05 mm before you even start. Probe the rotary center with a test bar and a dial indicator. Write the value down. Do not rely on the factory sticker.
Step-by-Step: Integrating the Fourth Axis Without Breaking Your Process
Here is the sequence we follow for every new rotary installation.
- Probe and document the rotary centerline. Mount a precision test bar in the chuck. Sweep it with a dial indicator at two points along its length. Adjust the A-axis zero until runout is under 0.01 mm. Record the Y and Z offsets in your setup sheet.
- Verify postprocessor direction and limits. Command A+45° from MDI. Watch the chuck. Confirm it turns clockwise (right-hand rule around +X). Then command A-45°. If direction is wrong, edit the postprocessor factor before running any CAM output [citation:2].
- Set soft limits for continuous rotation. Many controllers default to 360° travel. Continuous milling of helical features often needs 720° or more. Adjust the A-axis maximum travel parameter to at least 720,000 (in degrees) to avoid mid-cut overtravel alarms [citation:7].
- Run a dry-cut simulation with the actual G-code. Do not trust CAM internal simulation alone. Load the post-processed code into a verifier that models machine kinematics. Check for rotary overtravel, tool holder collisions with the chuck, and unexpected axis flips near the centerline.
- Cut a sacrificial test part. Use inexpensive stock. Machine a simple radial pattern and a helical groove. Measure feature positions relative to the rotary center. Adjust work offsets if needed. Only then run the real part.
Where the 4 Axis cnc milling machin Fits in 2026 Production
The fourth axis sits in a sweet spot. A 5-axis machine costs 40–60% more and demands programmers who understand singularity avoidance and tool vector control. A 3-axis machine cannot touch cylindrical or multi-face geometry without repeated setups.
For job shops running mixed batches of brackets, shafts, and housings, the 4 axis cnc milling machin delivers 80% of the multi-face capability at 50% of the 5-axis price. That is the pragmatic choice.
Surface finish also improves in continuous mode. When the A-axis rotates the workpiece while the cutter engages, the tool maintains a consistent contact angle. The step-over marks that plague 3-axis multi-setup work disappear. RapidDirect’s comparison notes that 4-axis operations can reach surface roughness values around Ra 0.4 µm with proper tool orientation, versus 1.6 µm typical for 3-axis multi-setup work [citation:13].
Frequently Asked Questions
What is the difference between 3+1 and true 4-axis simultaneous machining?
3+1 (indexed) locks the rotary axis at a fixed angle while cutting, then rotates to the next position. True simultaneous mode moves the A-axis while the X/Y/Z axes cut. Indexed suits radial bolt patterns and flat features at angles. Simultaneous suits helical grooves, cams, and spiral contours. Most entry-level rotary tables support both; the CAM strategy decides which you use.
Can I add a 4 axis cnc milling machin rotary table to my existing 3-axis VMC?
Usually yes, if your controller has a spare servo axis and your CAM software supports rotary toolpaths. Check three things: servo drive capacity, controller axis count license, and whether your postprocessor library includes the rotary configuration. The wiring is straightforward. The postprocessor validation is where most retrofits fail.
How do I choose between a trunnion table and a standalone rotary table for 4 axis milling?
A standalone rotary table mounts on the existing machine table and rotates the workpiece around the X-axis. It is cheaper and easier to remove for 3-axis work. A trunnion integrates the rotary into the machine structure, offering better rigidity and usually a larger swing diameter. For production runs of cylindrical or multi-face parts, trunnion rigidity wins. For mixed high-mix low-volume work, a removable rotary table preserves flexibility.
What tolerance can a 4 axis cnc milling machin hold on radial features?
Typical positioning accuracy on a quality rotary table is ±0.01° to ±0.02°. At a 100 mm radius, that translates to roughly ±0.017 to ±0.035 mm of arc length error. Combined with linear axis accuracy, a well-maintained 4-axis setup holds ±0.05 mm on radial hole patterns without special compensation. Tighter than that requires thermal stabilization and in-process probing.
Does the fourth axis reduce tool life or increase vibration?
It can, if you run continuous rotary cuts with a long tool at high feed. The rotary motion adds a tangential velocity component that changes the effective chip load. Start with 20–30% lower feed than the equivalent linear cut, then ramp up. Rigid workholding and a preloaded rotary table eliminate most vibration issues. A loose chuck is the most common culprit behind poor finish on 4-axis work.
Checklist: Before You Commit to a 4-Axis Solution
Use this list before signing a purchase order or scheduling the first job.
- ☐ Part audit complete: at least 30% of your current work requires 3+ faces or rotary geometry.
- ☐ Rotary centerline probed and documented to under 0.01 mm runout.
- ☐ Postprocessor direction verified against controller with an air cut.
- ☐ A-axis soft limit set to at least 720° for continuous milling.
- ☐ Full G-code simulation completed with machine kinematics model.
- ☐ Sacrificial test part cut and measured before production release.
- ☐ Operator trained on rotary coordinate systems and chuck safety.
- ☐ Chip containment and coolant direction checked for rotary operations.