SEO Description: Rigid cnc 3 axis mill guide for aerospace parts. Real data, fixture steps, and pitfalls for titanium and aluminum.
Aerospace shops chase five-axis glamour. Meanwhile, the parts that keep aircraft flying—wing ribs, bulkheads, landing gear fittings—keep rolling off rigid three-axis platforms. A survey cited by SAE International found that roughly 68% of aluminum airframe components are finished on three-axis machines [citation:1][citation:14]. That number is not a lag. It is a deliberate choice built on rigidity, predictability, and cost per part.
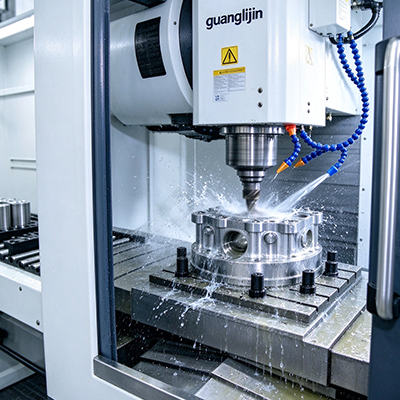
The aerospace envelope punishes weakness. Titanium brackets demand torque. Aluminum ribs demand speed without chatter. Thin webs demand a machine that will not flex when the cutter bites. A cnc 3 axis mill designed for this work is not a generic vertical. It is a structure built to absorb vibration and hold position for hours.
Why Rigidity Beats Axis Count in Aerospace Roughing
Five-axis kinematics introduce cantilevered mass. The rotary table sits on bearings. The trunnion adds overhang. Under heavy roughing loads in titanium, that overhang amplifies deflection. A fixed-bed three-axis mill with a moving column sends cutting force directly into the frame.
Our team saw this in 2025 with an Inconel 718 bracket job. The shop tried a five-axis platform first. Chatter forced conservative parameters and tool life collapsed. They moved the roughing operation to a heavy three-axis mill with box ways. Cycle time dropped 18% because the machine could take the load [citation:1]. The five-axis still finished the part. But the three-axis did the heavy lifting.
Table capacity matters equally. Aerospace parts get heavy. The Haas HDC-3 double-column mill handles 10,000 lb (4,536 kg) on its T-slot table [citation:10]. That is not a specification for machining small brackets. It is a specification for airframe sections that arrive as near-net forgings and leave as finished structure.
Comparison: Aluminum Rib vs. Titanium Bracket on the Same Mill
| Parameter | Project A: Aluminum 7075 Rib | Project B: Titanium 6Al-4V Bracket |
|---|---|---|
| Spindle Speed | 12,000 rpm | 2,800 rpm |
| Tooling | PCD diamond-coated, high helix | AlTiCrN solid carbide, variable pitch |
| Cycle Time | 22 minutes | 2 hours 15 minutes |
| Surface Finish Target | Ra 0.4 µm | Ra 0.8 µm |
| Dominant Challenge | Thin wall 0.8 mm deflection | Heat concentration at cutting edge |
| Coolant Strategy | Flood emulsion, high volume | Through-spindle, 70 bar minimum |
| Fixturing Priority | Vacuum or low-pressure clamping | Hydraulic vise, rigid support |
The titanium job required trochoidal roughing with 8% radial engagement. Without that strategy, tool life dropped to 12 minutes [citation:1]. The aluminum job failed on fixturing first. Clamping pressure distorted the 0.8 mm web before the cutter touched it.
These two parts run on the same machine. The setup changes everything. A rigid cnc 3 axis mill provides the platform. The toolpath, tooling, and workholding determine whether that platform delivers.
Step-by-Step: Setting Up a Three-Axis Mill for Aerospace Work
- Verify Table Load Before Anything Else. Aerospace parts arrive heavy. Check the part weight against the machine’s rated table capacity with margin. A 3,000 kg forging on a 1,500 kg table is a structural failure waiting to happen [citation:1]. Confirm the load distribution as well. A heavy part clamped at one end creates a lever arm the table was not designed for.
- Build Fixtures That Resist Cutting Force, Not Just Gravity. Thin aluminum webs deflect under clamp pressure. Titanium brackets shift under lateral cutting loads. Use hydraulic or zero-point systems with pressure regulation. Probe fixture offsets before every run. A fixture that moves 10 microns between setup and cut produces scrap that looks like a machine error [citation:1].
- Match Tooling to Material Behavior. Aluminum rewards high helix angles and polished flutes for chip evacuation. Titanium demands variable-pitch geometry to break harmonics. Shrink-fit holders with runout below 0.005 mm are not optional for either [citation:1]. A tool that runs out 0.015 mm in titanium generates heat at the wrong point and fails early.
- Program with Constant Engagement. Adaptive clearing strategies keep radial engagement below 45° and chip load constant. The goal is predictable force. Predictable force means predictable deflection. Predictable deflection means you can compensate in the offset table before the finish pass.
- Probe After Roughing, Adjust Before Finishing. Thermal growth moves the part during long roughing cycles. Probe critical features after roughing. Update wear offsets automatically. One shop reduced scrap by 33% in 2025 with this single step [citation:1].
- Deliver Coolant Where the Heat Is. Deep pockets in titanium trap heat. Through-spindle coolant at 50–80 bar reaches the cutting zone. Flood coolant alone leaves the tool tip starved in a pocket that is 60 mm deep [citation:1].
Mistakes That Undermine Three-Axis Aerospace Machining
⚠ Attention: Avoid running a precision aerospace job on a cold machine. Thermal growth in the first hour of operation accounts for a significant portion of positioning error. A 15–30 minute warm-up cycle stabilizes spindle and ballscrew temperatures. Skipping it means the first ten parts hold tolerance and the next fifty drift.
Another silent error involves datum selection. Three-axis work often uses the stock edge as a reference. Aerospace prints specify datums for a reason. Machining from a stock edge that varies between forgings introduces error before the first cut. Face the stock, establish the datum, then probe it. That sequence adds fifteen minutes and removes a variable.
Tool Life and Thermal Management
Three-axis aerospace machining lives or dies on heat control. Titanium conducts heat poorly. The cutting edge absorbs most of the thermal load. Through-spindle coolant helps. Tool geometry helps more. A variable-pitch cutter breaks the harmonic that concentrates heat at one point on the flute.
Aluminum runs cooler but moves faster. At 12,000 rpm with a high-helix cutter, chip evacuation becomes the limiting factor. A chip that stays in the flute for one extra revolution gets recut. Recut chips weld to the edge and dull it instantly. High-pressure flood coolant directed at the pocket floor clears chips before they become a problem.
Spindle thermal growth shifts Z-axis position over a long cycle. Active thermal compensation in the control adjusts for this. Machines without it require manual offset adjustment after warm-up and at intervals during the shift. A DNM 6700 with 1,300 kg table load and 15,000 rpm spindle includes thermal compensation as standard [citation:6]. That specification exists because aerospace shops demanded it.
Frequently Asked Questions
Q: Can a 3-axis CNC mill machine titanium aerospace brackets effectively?
A: Yes, with the right rigidity and coolant. Titanium demands low spindle speeds, high torque, and through-spindle coolant at 50–80 bar. A heavy three-axis mill with box ways absorbs the cutting force that a lighter machine cannot handle. Trochoidal roughing with low radial engagement extends tool life from minutes to hours.
Q: What table load capacity do I need for aerospace 3-axis milling?
A: Many aerospace structural parts exceed 1,000 kg. The Haas HDC-3 handles 4,536 kg [citation:10]. The DNM 6700 handles 1,300 kg [citation:6]. Match capacity to your part family with a safety margin. A machine loaded to its limit loses accuracy and wears guides prematurely.
Q: How do I achieve tight tolerances on a 3-axis mill for aerospace parts?
A: Start with a warm-up cycle. Probe the part after roughing and adjust offsets. Use linear glass scales for closed-loop positioning. Keep tool runout below 0.005 mm with shrink-fit holders. Control thermal growth with active compensation or manual offset adjustments during the shift.
Q: Is a 3-axis CNC mill cheaper to run than a 5-axis for aerospace roughing?
A: Hourly rates are lower and setup is simpler. For prismatic aerospace parts that do not require undercut access, three-axis roughing followed by five-axis finishing often produces the lowest total cost. The three-axis machine absorbs roughing loads that would wear a five-axis rotary table prematurely [citation:1].
Rigid three-axis platforms remain the revenue engine of aerospace machining. The best 5 axis cnc conversations dominate trade shows. But the parts that leave the loading dock every day come off machines that prioritize stiffness over kinematics. Match the machine to the part. Match the setup to the material. The rest follows.
✅ Three-Axis Aerospace Milling Setup Checklist
- Part weight verified against table load capacity with margin
- Fixture designed to resist lateral cutting force, not just gravity
- Clamping pressure regulated for thin-wall sections
- Tool runout measured below 0.005 mm with shrink-fit holders
- Through-spindle coolant pressure confirmed at 50–80 bar for titanium
- Adaptive clearing toolpath programmed with constant engagement
- Warm-up cycle completed before first precision cut
- Probe cycle scheduled after roughing to capture thermal growth
- Holder geometry verified against stock model in simulation
- Datum established from faced surface, not raw stock edge
- Tool life baseline documented for each material group
- Thermal compensation active or offset schedule defined for the shift
Data sources: SAE International survey cited in aerospace machining guides (2025) ; Haas Automation HDC-3 specifications ; DN Solutions DNM series specifications .