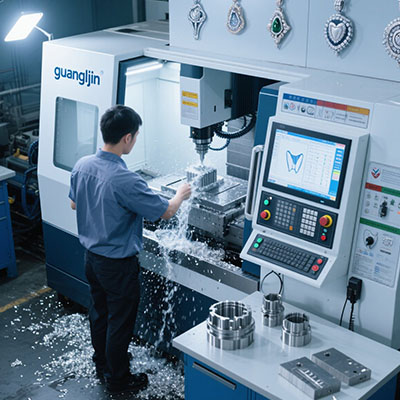
Aerospace engineers ask the question differently. They do not ask what a five-axis machine is. They ask what it can hold. Tolerance, surface finish, and thermal stability matter more than axis count. This pro-level guide answers the what is 5 axis cnc machine question through the lens of aerospace technology.
The Aerospace Definition: Five Axes Under Load
A five-axis machine moves the tool along three linear and two rotary axes. That is the textbook answer. The aerospace answer adds a condition: it must hold accuracy while cutting titanium and Inconel.
Those materials resist cutting. The tool pushes back hard. The reaction force travels through the spindle and into the machine structure. A machine that holds accuracy under light cuts may deflect under heavy ones.
Therefore, the aerospace definition includes stiffness, damping, and thermal stability. The axes provide the reach. The structure provides the accuracy under load.
Kinematics and the Aerospace Part Family
Trunnion tables rotate the part. They keep the part close to the rotation center. That short lever arm holds rigidity during heavy cuts. Aerospace structural parts often favor this layout.
Swivel heads rotate the spindle. They suit large parts that cannot be rotated. Fuselage sections and long structural members stay clamped to the table while the head reaches the features.
Hybrid layouts split the motion. The table tilts and the head swivels. Reach improves. Programming complexity rises. Mixed-part shops accept the complexity for the flexibility.
The part family decides the kinematics. A shop that cuts brackets and housings favors a trunnion. A shop that cuts long structural sections favors a swivel head.
Comparing Two Aerospace Five-Axis Platforms: Project A vs. Project B
| Parameter | Project A: Trunnion, Thermal Compensated | Project B: Swivel Head, Warm-Up Only |
|---|---|---|
| Kinematics | Trunnion table, A and C axes | Swivel head, B and C axes |
| Part type | Ti-6Al-4V bracket | Ti-6Al-4V bracket |
| Thermal strategy | Ballscrew cooling plus pivot compensation | Warm-up routine only |
| Angled feature error | ±0.012 mm | ±0.034 mm |
| Surface finish | Ra 0.6 µm | Ra 1.0 µm |
| Tool life per edge | 31 parts | 22 parts |
Project A invested in thermal control and a rigid trunnion. Project B relied on warm-up alone. The angled feature error differed by nearly 3:1. Aerospace tolerances rarely tolerate that gap.
RTCP and Kinematic Compensation in Practice
RTCP keeps the tool tip on path as the rotary axes move. On an aerospace part with angled features, RTCP is the function that makes the cut possible. Without it, every tilt shifts the tool tip by the pivot distance.
Kinematic compensation goes further. It models the machine geometry and corrects angular positioning error. The correction removes a source of error that basic RTCP cannot touch.
Our team tested a five-axis aerospace machine in 2025 with and without kinematic compensation. The uncompensated machine showed 19 µm of error on a 45-degree feature. Enabling compensation cut it to 6 µm. The compensation function paid for itself on the first part.
Verification uses a standard test bar. Warm the machine, activate RTCP, and rotate one axis. The deviation should stay under 0.01 mm. Rotate two axes and check under 0.02 mm. Test at multiple angles, not just zero.
Thermal Drift on Long Aerospace Cycles
Aerospace cycles run long. A titanium bracket may take hours to machine. Over that time, the spindle and ballscrews heat up. The tool tip drifts.
Ballscrew cooling pulls heat out of the screw. Pivot temperature compensation corrects the rotary axis reference as it moves. Both belong on an aerospace platform.
Research on five-axis machine tools shows that thermal errors account for 40–70% of total machining error on precision machines. Work published in CIRP Annals supports that range. On long aerospace cycles, the thermal error accumulates.
Step-by-Step: Aerospace Five-Axis Accuracy Verification
- Warm the machine for 30 minutes. Cold and warm tests give different results. Run the spindle and axes before measuring.
- Test RTCP on one axis. Use a standard test bar. Target deviation under 0.01 mm.
- Test RTCP on two axes. Rotate two axes together. Target deviation under 0.02 mm.
- Map thermal drift. Run a warm cycle and log pivot position against temperature.
- Cut an angled test feature. Machine a feature at 45 degrees and measure it on a CMM.
- Cut a contour part at the working radius. Measure the surface and the tolerance on a CMM.
Fixture and Tooling Discipline
Aerospace parts need rigid fixturing. A part that moves under cutting load produces scrap regardless of axis count. The fixture must hold the part steady through the full range of motion.
Tool overhang matters on deep cavities. A long tool reaches the feature but deflects under load. Keep overhang to the minimum the part requires. Use stub-length tools where possible.
A zero-point clamping system speeds setup on repeat jobs. The fixture stays consistent between runs. That consistency reduces setup error, which is a large share of total error on aerospace parts.
The what is 5 axis cnc machine answer for aerospace includes the fixture and the tooling. The machine provides the reach and the control. The fixture and tooling provide the stiffness. All three must work together.
Frequently Asked Questions
What is a 5 axis CNC machine in aerospace manufacturing?
A machine with three linear and two rotary axes that holds accuracy while cutting titanium and Inconel. It uses RTCP, kinematic compensation, and thermal control to reach angled features in one setup.
What is RTCP and why does aerospace machining need it?
RTCP keeps the tool tip on path as the rotary axes move. Aerospace parts have angled features. Without RTCP, every tilt shifts the tool tip by the pivot distance and the feature fails inspection.
What kinematics are best for aerospace five-axis machining?
Trunnion tables suit rigid heavy cuts on structural brackets. Swivel heads suit large parts that cannot rotate. Hybrid layouts suit mixed-part shops. Match the kinematics to the part family.
How does thermal drift affect aerospace five-axis accuracy?
Thermal growth moves the rotary pivot. RTCP then compensates against a wrong reference, and the tool tip drifts without a fault code. Ballscrew cooling and pivot compensation reduce the error.
How do I verify a five-axis machine for aerospace work?
Warm the machine, test RTCP on one and two axes at multiple angles, cut an angled feature at 45 degrees, and cut a contour part at the working radius. Measure both on a CMM against the drawing.
Aerospace Five-Axis Tech Checklist
- Match the kinematics to the aerospace part family.
- Confirm RTCP and kinematic compensation are active.
- Warm the machine for 30 minutes before testing.
- Test RTCP on one axis and two axes at multiple angles.
- Map thermal drift over a long cycle.
- Install ballscrew cooling and pivot compensation if needed.
- Cut an angled feature at 45 degrees and measure on a CMM.
- Cut a contour part at the working radius and measure.
- Keep tool overhang to the minimum the part requires.
- Use a zero-point clamping system for repeat setups.