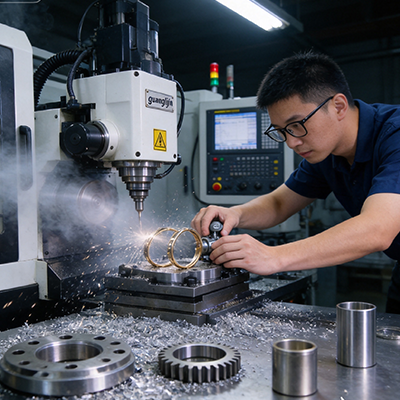
Small machines are not small versions of large machines. They have their own error profile. Short travels hide some errors and amplify others. A precision kit for a small 3-axis CNC machine targets the errors that actually show up on small parts. This guide covers what belongs in the kit and how to use it.
Why Small Machines Need a Different Precision Approach
A small machine has short travels. Accumulated linear error stays low. That is good news. However, the light frame flexes more under cutting load. That is the bad news.
The error profile shifts toward stiffness and tram. A small column deflects under load. The spindle tilts out of tram. The part shows taper and step marks that a larger machine would not produce.
Therefore, the precision kit for a small 3 axis cnc machine focuses on tram, gib adjustment, backlash, and workholding rigidity. Linear accuracy matters, but it is rarely the limiting factor on a short-travel machine.
What Belongs in a Precision Kit
A useful kit is short and specific. A dial test indicator with a magnetic base covers tram and runout. A granite square checks column squareness. Feeler gauges handle gib adjustment. A precision level checks the bench and the table.
A backlash test bar or a simple dial indicator setup measures lost motion on each axis. A torque wrench handles bearing preload and bolt tightening. A set of brass shims corrects small misalignments without scraping.
Software belongs in the kit too. A simple probing routine or a touch-off macro speeds setup. A spreadsheet for tracking backlash and tram over time shows wear trends before they cause scrap.
Our team built precision kits for a small-parts shop in 2025. The shop had been chasing taper on aluminum parts for weeks. The kit found the spindle out of tram by 0.04 mm over 150 mm. Correcting the tram removed the taper in one afternoon. The parts had been blamed on tool wear.
Comparing Two Small Machine Setups: Project A vs. Project B
| Parameter | Project A: Precision Kit Applied | Project B: Factory Setup Only |
|---|---|---|
| Spindle tram | Verified and corrected to 0.01 mm over 150 mm | Factory setting, not verified |
| Gib adjustment | Set with feeler gauge, checked for stick-slip | Factory setting |
| Backlash | Measured and reduced under 8 µm per axis | Not measured |
| Bench rigidity | Machine bolted to a leveled rigid bench | Set on a light table |
| Taper on 100 mm part | Under 0.01 mm | 0.04 mm |
| Surface finish | Ra 0.8 µm on aluminum | Ra 1.6 µm with visible chatter |
Project A spent a day applying the kit and got a machine that cut straight. Project B trusted the factory setup and fought taper and chatter for weeks. The kit cost less than the scrap from one bad batch.
Tram: The First Check on Any Small Machine
Tram is the spindle axis relative to the table. A machine out of tram cuts a taper and leaves a step when the tool changes direction. On a small machine, the light column makes tram drift more likely.
Check tram with a dial test indicator on a spindle-mounted arm. Sweep the indicator around a circle on the table. The reading difference across the circle is the tram error. Check it at two radii to separate tilt from a bent arm.
Correct tram by shimming the column base or adjusting the column mounting bolts. Make small changes and re-check. A 0.01 mm shim moves the tram by a predictable amount. Record the shim thickness and the resulting tram for future reference.
Re-check tram after any crash or heavy cut. A small machine moves more than a large one. A bump that would not affect a heavy machine can shift a light column.
Gib Adjustment and Backlash
Dovetail ways use gibs to control play. A loose gib lets the table rock. A tight gib causes stick-slip and wear. The right setting is snug but free-moving.
Adjust the gib with a feeler gauge and a test move. Tighten until the table feels stiff, then back off slightly. Run the axis through its full travel. It should move smoothly without binding at the ends.
Backlash on a small machine often comes from the leadscrew nut or the ballscrew nut. Measure it with a dial indicator against the table. Command a small move in one direction, then reverse. The difference between the indicator reading and the commanded move is the backlash.
Adjust the nut preload in small increments. Over-tightening accelerates wear. After adjustment, run the axis through its travel and re-check. Record the value in the maintenance log.
Step-by-Step: Applying the Precision Kit
- Level the bench and bolt the machine down. A light machine on a flexible bench transfers vibration into the cut.
- Check spindle tram. Sweep a dial test indicator around a circle on the table at two radii. Record the error.
- Correct tram with shims. Make small changes and re-check until the error is under 0.01 mm over 150 mm.
- Adjust the gibs. Set each axis snug but free-moving. Run the full travel to check for binding.
- Measure and adjust backlash. Check each axis with a dial indicator. Adjust the nut preload in small increments.
- Cut a test part. Machine a stepped block and measure taper, squareness, and step height on a CMM.
- Log all values. Record tram, gib settings, and backlash for future comparison.
Workholding and Tooling on a Small Machine
Small machines cut small parts. Workholding must be rigid and compact. A small vise with a solid base holds better than a large vise with overhang. A fixture plate bolted to the table adds stiffness.
Tool overhang matters more on a small machine. A short tool is stiff. A long tool deflects and chatters. Keep overhang to the minimum the part requires. Use stub-length tools where possible.
Tool holders should match the spindle taper and the tool shank. A loose holder adds runout. Measure runout at the tool tip. Target under 0.01 mm for small end mills.
Research on small machine tools shows that stiffness and tram dominate part error when travels are short. Work published on compact machining platforms supports that finding. The precision kit targets exactly those error sources.
The small 3 axis cnc machine rewards owners who apply the kit and log the results. Tram, gibs, backlash, and workholding decide whether the machine cuts straight. The kit supplies the tools. The log supplies the discipline.
Frequently Asked Questions
What belongs in a precision kit for a small 3 axis CNC machine?
A dial test indicator with a magnetic base, a granite square, feeler gauges, a precision level, a backlash test setup, a torque wrench, and brass shims. Add a simple probing routine and a tracking spreadsheet.
How do I check spindle tram on a small CNC machine?
Mount a dial test indicator on a spindle arm. Sweep it around a circle on the table at two radii. The difference across the circle is the tram error. Correct it with column shims and re-check.
What causes taper on a small 3 axis CNC machine?
Spindle tram is the usual cause. A light column drifts out of tram under cutting load. A 0.04 mm tram error over 150 mm produces visible taper on a 100 mm part. Re-check tram after any crash.
How much backlash is acceptable on a small CNC machine?
Target under 8 µm per axis for small-part work. Higher backlash produces steps on direction changes. Adjust the nut preload in small increments and re-check through the full travel.
Why does a small CNC machine chatter more than a large one?
The frame is lighter and deflects more under load. Check bench rigidity first. Then check tram, gib adjustment, and tool overhang. Keep tools short and the workholding rigid.
Small 3-Axis Precision Kit Checklist
- Level the bench and bolt the machine down.
- Check spindle tram at two radii and record the error.
- Correct tram with shims until under 0.01 mm over 150 mm.
- Set gibs snug but free-moving on each axis.
- Measure backlash on each axis with a dial indicator.
- Adjust nut preload in small increments and re-check.
- Check tool runout at the tip and target under 0.01 mm.
- Keep tool overhang to the minimum the part requires.
- Cut a stepped test block and measure taper and step height.
- Log tram, gib settings, and backlash for future comparison.