SEO Description: Advanced cnc 3 axis mill machining for aerospace. High-speed spindles, adaptive toolpaths, and real shop data.
Aerospace machining does not reward brute force alone. A 40-taper spindle at 8,000 rpm will remove metal from an aluminum rib. It will also chatter, burn through tools, and leave a finish that fails inspection. Advanced three-axis machining is a system: spindle, toolpath, coolant, and monitoring working together.
The investment case is simple. Aerospace aluminum airframe components still run predominantly on three-axis platforms. A survey cited by SAE International put the figure near 68% . The machines advanced shops buy are not basic verticals. They carry high-speed spindles, adaptive control, and thermal compensation as standard equipment.
The High-Speed Spindle Decision
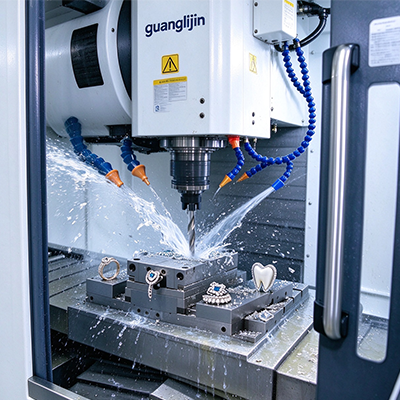
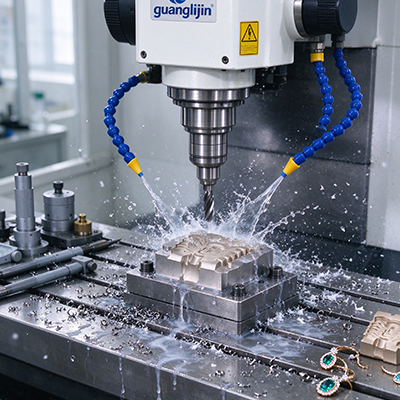
Spindle speed changes everything in aluminum. At 15,000 rpm with a 16 mm cutter, surface speed crosses 750 m/min. Chips leave the flute before heat migrates into the workpiece. Tool life extends. Surface finish improves. The cycle time on a typical rib drops measurably.
Titanium is the opposite story. High speed is wrong for roughing. Torque at low rpm removes material without generating heat at the edge. Advanced shops keep two strategies on the same floor. The aluminum cell runs high-speed spindles. The titanium cell runs heavy 40-taper or HSK-A100 with high torque.
DN Solutions builds the DNM 6700 with a 15,000 rpm spindle and 1,300 kg table capacity . That combination covers aluminum finishing and moderate titanium work. For pure titanium roughing, a box-way machine with lower top speed delivers better results. The best 5 axis cnc platforms often handle finishing, while three-axis machines do the heavy removal.
Comparison: Two Advanced Three-Axis Strategies
| Parameter | Project A: High-Speed Aluminum Cell | Project B: Heavy Titanium Roughing Cell |
|---|---|---|
| Spindle | 15,000–24,000 rpm, HSK-A63 | 6,000–8,000 rpm, high torque, BT50 |
| Structure | Cast iron, linear guides | Box ways, cast iron base |
| Toolpath Strategy | High-speed trochoidal, 45° engagement | Adaptive roughing, 8% radial engagement |
| Coolant | Flood at 40–60 bar, chip evacuation priority | Through-spindle at 70+ bar, heat priority |
| Typical Part | Wing rib, 0.8 mm web | Landing gear fitting, 150 kg forging |
| Cycle Time Driver | Chip load and surface speed | Tool life and cutting force |
| Monitoring Need | Spindle load, chip evacuation | Tool wear, vibration, thermal growth |
Project A lives on speed. Project B lives on force control. Mixing the two on one machine produces compromise. Advanced shops separate the cells and tune each setup to its material.
Step-by-Step: Advanced Three-Axis Setup for Aerospace
- Profile the Spindle Load During Roughing. Record spindle load on every roughing pass. A load that spikes above 80% of rated power signals engagement problems or tool wear. Stable load within 60–75% means the toolpath is controlling force, not fighting it .
- Program Adaptive Clearing With Constant Chip Load. Keep radial engagement below 45° and chip load constant. The goal is predictable force. Predictable force means predictable deflection. Predictable deflection can be compensated before the finish pass.
- Deploy Through-Spindle Coolant for Titanium. 70 bar minimum. The coolant must reach the cutting edge, not the pocket wall. Deep pockets trap heat. Flood coolant alone leaves the tip starved.
- Probe After Roughing, Adjust Before Finishing. Roughing generates heat and relieves residual stress. The part moves. Probe critical datums after roughing. Update wear offsets automatically. One shop cut scrap 33% in 2025 with this step .
- Monitor Tool Wear With Spindle Load Trending. A gradual rise in spindle load at constant parameters signals tool wear. Set alarms at 15% above baseline. Change tools before the edge fails, not after the finish pass scrapes.
- Verify Thermal Stability at Shift Start. Run the warm-up cycle. Check spindle and ballscrew temperatures against the control’s thermal model. A machine that starts cold produces different parts than one that has run for two hours.
Mistakes That Limit Advanced Three-Axis Performance
⚠ Attention: Avoid using the same fixturing philosophy for aluminum and titanium. Aluminum thin walls deflect under clamp pressure. Titanium forgings resist clamping but shift under lateral cutting force. Each material demands its own fixture design, clamping sequence, and probe verification.
We worked with an aerospace supplier in 2025 that struggled with tool life on 7075 aluminum ribs. The toolpath was correct. The coolant was correct. The problem was runout. Their holders measured 0.012 mm at the tool tip. After switching to shrink-fit holders with 0.003 mm runout, tool life tripled. Cycle time dropped 22% because they could increase feed without chatter. The fix cost less than $15,000 in holders.
Monitoring and Data in Advanced Machining
Advanced machining generates data. Spindle load, coolant pressure, vibration sensors, and probe results all feed the control. Shops that use this data catch problems early. Shops that ignore it discover problems in inspection.
Spindle load trending is the simplest tool. Record load on every cycle. Plot it over weeks. A rising trend at constant parameters means wear somewhere in the system. The tool, the fixture, or the spindle itself. Finding the source early saves scrap.
Vibration monitoring catches chatter before it damages the surface. An accelerometer on the spindle housing detects the frequency shift that precedes chatter. The control can reduce feed or change spindle speed automatically. The best cnc 3 axis mill platforms integrate these sensors as standard options.
Thermal monitoring closes the loop on accuracy. Spindle and ballscrew temperatures drive compensation models. The control adjusts positions in real time. Without monitoring, the model drifts from reality and the compensation becomes wrong.
Toolpath Strategy for Thin-Wall Aerospace Parts
Thin walls deflect. Aluminum ribs with 0.8 mm webs move under cutting force. The tool pushes. The wall springs back. The next pass cuts less than programmed. The result is a tapered wall that fails inspection.
Advanced strategies solve this. Alternate the cutting direction on each depth pass. Climb mill one side, conventional mill the other. The deflection balances. The wall stays parallel. Add a finishing pass with light radial engagement and high spindle speed. The force drops and the wall relaxes to its true position.
Fixture design matters equally. Vacuum fixturing distributes clamping force across the part. Low-pressure hydraulic clamping reduces distortion. Probe the clamped part before cutting. Measure the wall after roughing. Adjust the finishing toolpath to the measured condition. This is advanced three-axis work: sensing, deciding, adjusting.
Frequently Asked Questions
Q: What spindle speed is best for advanced 3-axis CNC machining of aluminum aerospace parts?
A: 15,000 to 24,000 rpm with HSK-A63 tooling for finishing and light roughing. Higher speed reduces cutting force and improves surface finish. The limiting factor is holder balance and tool runout, not the spindle itself.
Q: How do I reduce tool wear in titanium 3-axis milling?
A: Use adaptive roughing with low radial engagement, through-spindle coolant at 70 bar or higher, and variable-pitch carbide tools. Keep cutting force predictable. Probe the part after roughing to avoid recutting work-hardened material.
Q: What is adaptive clearing and why does it matter for aerospace machining?
A: Adaptive clearing maintains constant chip load and controlled radial engagement. The toolpath adjusts to the material condition. Force stays predictable. Tool life extends and surface finish improves, especially in deep pockets and thin-wall sections.
Q: How do I verify accuracy on an advanced 3-axis mill for aerospace work?
A: Run a ballbar test for contouring performance. Probe a certified master artifact. Trend spindle load and thermal data over time. Cut a test part, measure it, and compare against the machine’s reported position .
Advanced three-axis machining is not one feature. It is the combination of high-speed capability, adaptive toolpath control, coolant strategy, and data monitoring. Aerospace shops that treat these as a system outperform shops that buy machines and hope.
✅ Advanced Three-Axis Machining Readiness Checklist
- Spindle load profiled on all roughing passes with alarm thresholds set
- Adaptive clearing programmed with constant chip load and engagement
- Through-spindle coolant confirmed at 70+ bar for titanium work
- Tool holder runout measured below 0.005 mm
- Holders balanced to spindle maximum rated speed
- Probe cycle scheduled after roughing for offset correction
- Spindle load and vibration data logged and trended
- Warm-up cycle completed before precision operations
- Fixture strategy matched to material behavior
- Thin-wall parts programmed with alternating direction passes
- Thermal compensation active and verified against measured growth
- Tool life baselines established per material and operation
Data sources: SAE International survey cited in aerospace machining guides (2025) ; DN Solutions DNM series specifications ; advanced machining process guidance (2025) .